Best Digestive Enzymes for Gluten and Dairy Intolerance: B2B Dairy Enzyme Complex Checklist
Compare dairy enzyme complexes for cheese, yogurt, and milk processing with pH, temperature, dosage, COA/TDS/SDS, QC, pilot, and cost-in-use criteria.
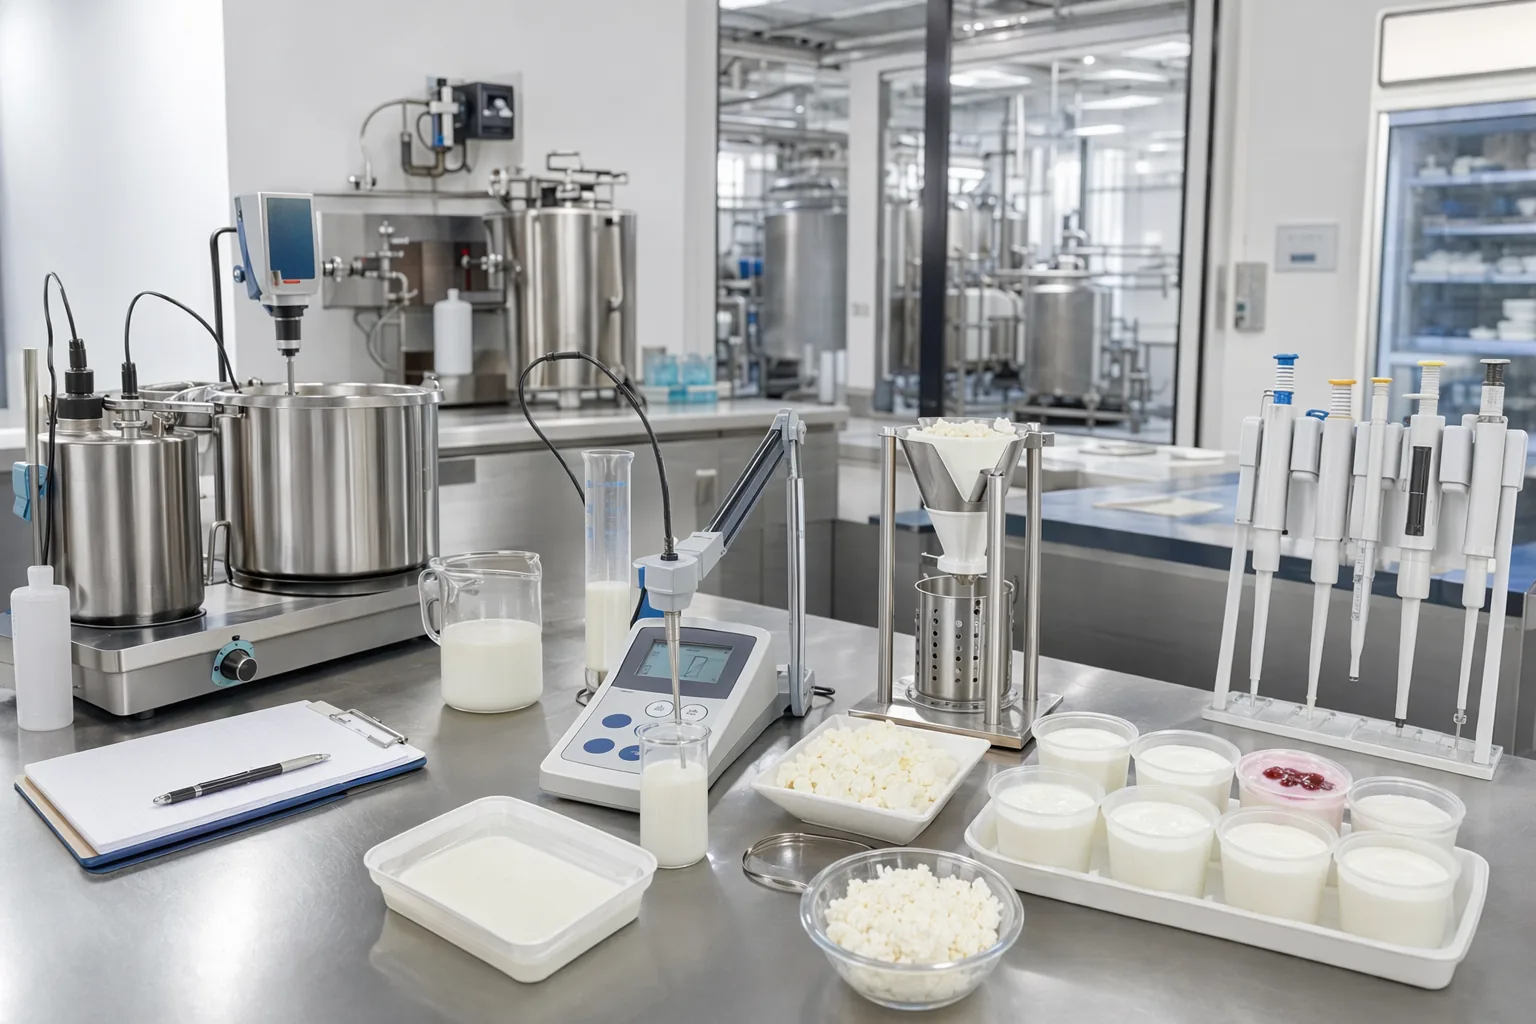
For dairy manufacturers, this comparison guide reframes consumer search language into industrial enzyme specifications for cheese, yogurt, and milk processing. It is written for buyers: dairy plants, ingredient resellers and brand owners who fill enzyme products, and it ends with what to send to request a quote.
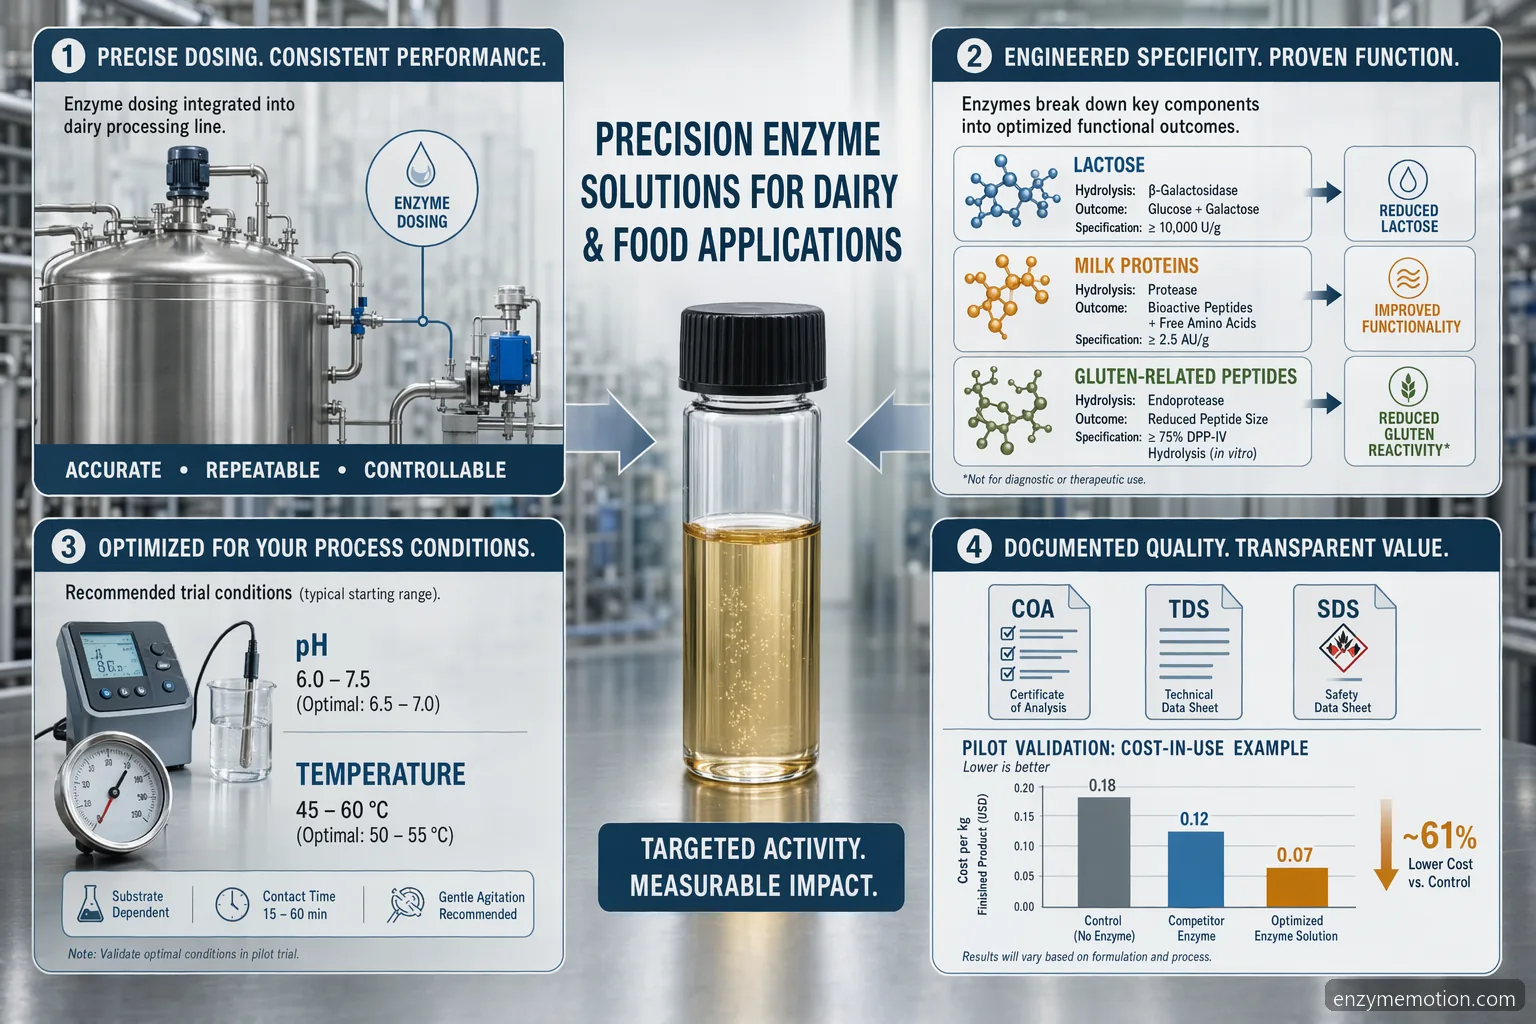
Why Consumer Search Terms Need Industrial Translation
Searches for the best digestive enzymes for gluten and dairy intolerance, digestive enzymes for dairy intolerance, or gluten dairy digestive enzymes usually point to consumer supplement decisions. A dairy processor has a different question: which enzyme complex performs predictably in milk, cream, cheese milk, yogurt base, or whey streams under controlled processing conditions? Industrial enzyme selection should not be based on medical positioning. It should be based on substrate specificity, declared activity units, process pH and temperature, contact time, inactivation options, sensory impact, and regulatory documentation for the target market. For dairy, common functions include lactase for lactose hydrolysis, protease for protein modification, lipase for flavor development, and microbial coagulants as rennet alternatives. If gluten-containing inclusions, grains, or flavors enter a dairy line, manage that through ingredient controls and allergen programs, not by assuming a dairy enzyme complex removes gluten risk.
Use consumer keywords only as demand signals, not specification criteria. • Define the industrial function before comparing suppliers. • Separate dairy processing performance from dietary or medical claims.
Match Enzyme Function to Cheese, Yogurt, and Milk Processing
A strong comparison starts with the application. In milk processing, lactase is commonly evaluated around pH 6.5 to 6.8 and chilled to moderate temperatures depending on the process, often with longer contact times at refrigeration temperatures or shorter holds at warmer conditions. In yogurt, the enzyme must tolerate formulation steps and should not interfere with culture acidification, viscosity, or post-acidification targets. In cheese, coagulant or protease systems must be assessed for flocculation time, curd firmness, moisture, yield, bitterness, and ripening behavior. Lipase may be valuable in specialty cheese flavor development, but it requires tight dosage control. A broad Dairy Enzyme Complex may be convenient, yet a single-function enzyme can be easier to validate. Ask suppliers whether activity is standardized for the intended substrate and whether performance data exists in comparable milk fat, protein, solids, and heat-treatment conditions.
Milk: lactose hydrolysis, sweetness balance, freezing-point considerations. • Yogurt: culture compatibility, viscosity, acidification profile. • Cheese: coagulation, proteolysis, yield, flavor, and texture control.
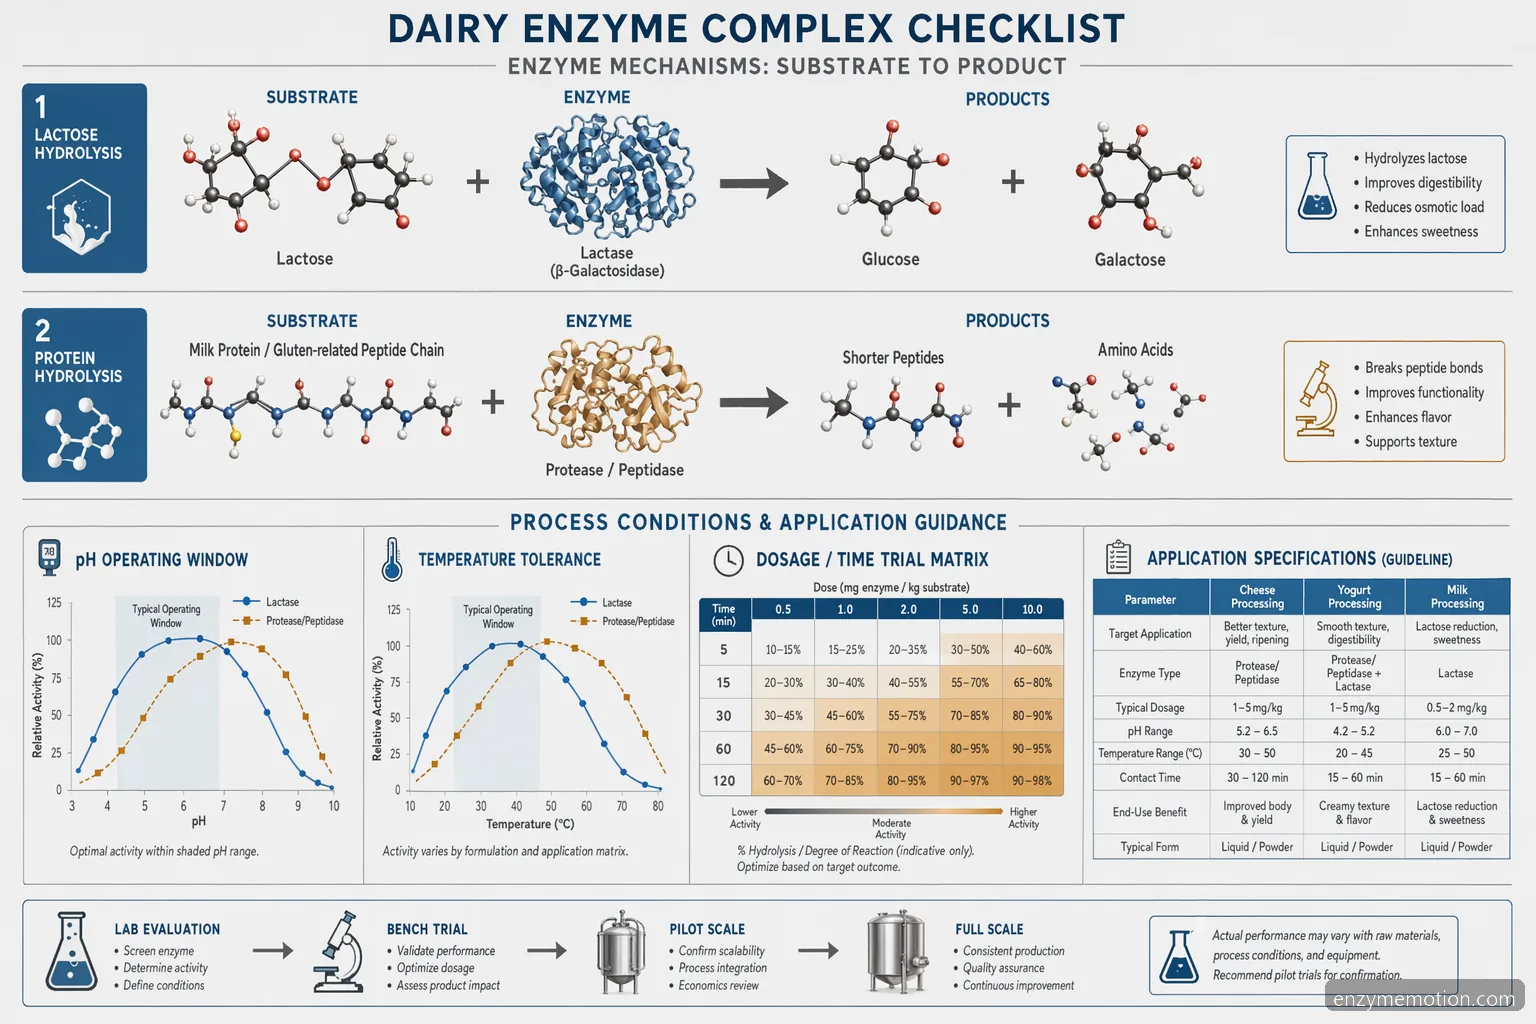
Process Conditions to Request Before a Trial
Before requesting samples, document your operating window and ask the supplier to confirm where the enzyme is expected to work. Typical dairy enzyme evaluations may include pH 6.4 to 6.8 for fluid milk lactase use, pH 4.4 to 4.8 for acidified yogurt environments, and cheese-milk temperatures near 30 to 37 degrees Celsius for many coagulation trials. Dosage bands vary widely by activity unit and objective, but pilot screening often begins with supplier-recommended ranges such as 0.01% to 0.10% w/w or activity-based dosing per liter or kilogram of substrate. Do not convert dosage by weight alone unless activity units are equivalent. Confirm whether the enzyme is liquid or powder, its carrier system, solubility, optimal pH, thermal stability, and how it can be inactivated through pasteurization, cooking, pH shift, or time-temperature exposure.
Record pH, temperature, contact time, solids, fat, and protein level. • Compare activity-unit dosing, not only grams per batch. • Confirm inactivation strategy and residual activity risk.
Documentation: COA, TDS, SDS, and Supplier Qualification
B2B buyers comparing the best digestive enzymes for dairy intolerance or gluten free dairy free digestive enzymes should shift the evaluation toward documentation quality. Each lot should be supported by a Certificate of Analysis with activity, appearance, microbiological limits, and relevant contaminant checks. The Technical Data Sheet should define enzyme source, activity method, recommended process conditions, dosage guidance, storage, shelf life, and handling. The Safety Data Sheet should support worker safety, spill response, and PPE decisions. Also request allergen statements, food-grade suitability, country-of-origin information, and GMO status where relevant to your customer requirements. Supplier qualification should include change-control procedures, lot traceability, production capacity, lead times, packaging integrity, and complaint handling. Avoid relying on broad marketing claims unless they are supported by methods, test data, and specifications that your quality team can audit.
Require COA, TDS, SDS, allergen statement, and traceability. • Review lot-to-lot activity variation and release methods. • Assess change control, capacity, and lead-time reliability.
Pilot Validation and Cost-in-Use Comparison
The lowest enzyme price per kilogram is rarely the lowest cost-in-use. Build a pilot plan that compares at least two dosage levels, one control, and one process condition challenge such as lower temperature, shorter hold time, or higher solids. For lactase, track lactose reduction, glucose/galactose formation, sweetness impact, viscosity, microbial quality, and sensory stability. For cheese enzymes or a rennet alternative, measure coagulation kinetics, curd cut firmness, whey losses, moisture, yield, texture, and flavor over shelf life or ripening. For protease and lipase systems, monitor bitterness, free fatty acids, peptide profile where available, and batch variability. Calculate cost per finished kilogram, not cost per drum. Include enzyme dose, yield change, processing time, waste, cleaning impact, rejected batches, documentation burden, and supplier service. Only scale up after pilot results match your specification and quality release criteria.
Compare cost per finished kilogram or liter. • Use analytical, sensory, and operational endpoints. • Validate under real plant constraints before commercial adoption.
Troubleshooting Common Process Failures
When a Dairy Enzyme Complex underperforms, start with the process record before changing suppliers. Low activity may result from incorrect storage, expired lot age, heat exposure, chlorine or sanitizer carryover, poor mixing, or pH outside the enzyme’s working range. Overactivity can cause bitterness, excess sweetness, weak gel structure, thin yogurt body, rapid coagulation, or inconsistent flavor release. For lactase, verify lactose hydrolysis using HPLC, enzymatic lactose assays, or validated rapid methods. For cheese coagulants, track flocculation time, cut time, curd firmness, moisture, fat retention, and yield. For protease and lipase systems, run sensory panels and monitor free amino nitrogen, free fatty acids, or other fit-for-purpose markers. If a plant is evaluating digestive enzymes for dairy intolerance style product positioning, keep the technical file focused on measurable lactose reduction or ingredient control, not unverified digestive outcomes.
Check storage temperature and lot age before reformulating. • Confirm pH, temperature, mixing, and contact time at production scale. • Use analytical tests that match the enzyme’s intended function.
For Brand Owners: Check the Carrier, Not Only the Activity
Brand owners and contract packers who fill lactase or blended enzyme powders into sachets and capsules face a label risk that a dairy plant does not. A public complaint shows it: a buyer found whole milk powder declared in the ingredient list of a lactase sachet, which made the product unsuitable for their purpose. The enzyme was not the problem; the carrier was.
Before approving a lactase or blended enzyme powder for a product sold as dairy-free, ask the supplier to declare the carrier and any filler on the specification, confirm it for every lot, and check that your own label matches, because an enzyme made to work inside milk is not automatically right for a dairy-free product.
Ask for the full composition, not only the activity. • Match the carrier to the claim on your label. • Re-confirm whenever lots or carriers change.
Technical Buying Checklist
Buyer Questions
No. This page uses common search language such as digestive enzymes for gluten and dairy to guide industrial buyers toward proper dairy enzyme specification. It is not medical supplement advice and does not address diagnosis, treatment, or personal nutrition. Dairy processors should evaluate enzyme complexes by activity, process fit, documentation, pilot validation, and finished-product quality requirements.
No enzyme complex should be assumed to remove gluten risk from a dairy product or facility. If gluten-containing grains, flavors, stabilizers, or inclusions are used, manage them through supplier approval, allergen control, validated cleaning, segregation, testing where appropriate, and accurate labeling. Dairy enzymes can support milk processing functions, but they are not a substitute for allergen management.
Request a current COA for the lot, a TDS with activity units and process guidance, and an SDS for safe handling. Also ask for allergen statements, traceability details, storage and shelf-life information, GMO status where relevant, recommended dosage bands, and change-control procedures. These documents help quality, procurement, and operations compare suppliers consistently.
For cheese, compare flocculation time, curd firmness at cut, moisture, fat and protein retention, whey clarity, yield, texture, flavor, bitterness, and ripening behavior. Include a control batch and at least two dosage levels. A rennet alternative or protease should be judged on finished cheese performance, not only on coagulation speed or enzyme price.
Normalize quotes by activity delivered to the process and finished-product outcome. Compare dosage per batch, yield impact, processing time, waste, QC requirements, storage losses, packaging size, lead time, technical support, and documentation quality. The best option is usually the one with the lowest validated cost-in-use and the most reliable supplier qualification profile.
Related Search Themes
digestive enzymes for dairy intolerance, best digestive enzymes for gluten and dairy intolerance, best digestive enzymes for dairy intolerance, digestive enzymes for gluten and dairy, dairy gluten digestive enzymes, gluten free dairy free digestive enzymes
Dairy Enzyme Complex for Research & Industry
Need Dairy Enzyme Complex for your lab or production process?
ISO 9001 certified · Food-grade & research-grade · Ships to 80+ countries
Frequently Asked Questions
Is this page recommending consumer digestive enzymes for dairy intolerance?
No. This page uses common search language such as digestive enzymes for gluten and dairy to guide industrial buyers toward proper dairy enzyme specification. It is not medical supplement advice and does not address diagnosis, treatment, or personal nutrition. Dairy processors should evaluate enzyme complexes by activity, process fit, documentation, pilot validation, and finished-product quality requirements.
Can a dairy enzyme complex solve gluten-related labeling or allergen issues?
No enzyme complex should be assumed to remove gluten risk from a dairy product or facility. If gluten-containing grains, flavors, stabilizers, or inclusions are used, manage them through supplier approval, allergen control, validated cleaning, segregation, testing where appropriate, and accurate labeling. Dairy enzymes can support milk processing functions, but they are not a substitute for allergen management.
What documentation should we request before buying a dairy enzyme?
Request a current COA for the lot, a TDS with activity units and process guidance, and an SDS for safe handling. Also ask for allergen statements, traceability details, storage and shelf-life information, GMO status where relevant, recommended dosage bands, and change-control procedures. These documents help quality, procurement, and operations compare suppliers consistently.
What pilot tests are most useful for cheese enzyme selection?
For cheese, compare flocculation time, curd firmness at cut, moisture, fat and protein retention, whey clarity, yield, texture, flavor, bitterness, and ripening behavior. Include a control batch and at least two dosage levels. A rennet alternative or protease should be judged on finished cheese performance, not only on coagulation speed or enzyme price.
How should we compare enzyme quotes from different suppliers?
Normalize quotes by activity delivered to the process and finished-product outcome. Compare dosage per batch, yield impact, processing time, waste, QC requirements, storage losses, packaging size, lead time, technical support, and documentation quality. The best option is usually the one with the lowest validated cost-in-use and the most reliable supplier qualification profile.
What is the main risk when scaling from lab to plant?
The main risk is assuming that bench performance will transfer directly to production. Plant-scale mixing, temperature gradients, residence time, milk variability, culture interaction, and heat treatment can change enzyme performance. A controlled pilot or plant trial should capture actual pH, temperature, hold time, dosage, lot number, and QC results. Scale-up approval should be based on repeatable finished-product data.
What should we send to get a wholesale quote?
The product (Dairy Enzyme Complex or a custom blend), the application, the quantity per order or per month, the pack size (1 kg, 5 kg or 25 kg) and the destination country. Brand owners should add the carrier they need declared on the specification.
Wholesale and bulk supply: request a quote
Turn This Guide Into a Supplier Brief Request a Dairy Enzyme Complex specification review, sample plan, and pilot validation checklist for your process. Wholesale and bulk supply for dairy manufacturers, ingredient plants and resellers: send the product, the application, the quantity (per order or per month), the pack size (1 kg, 5 kg or 25 kg) and the destination country, and we respond within 24 hours.
Contact Us to Contributehello@mail.enzymemotion.com